
High Potent
- Constructed 2015
- Manufacturing since 2018
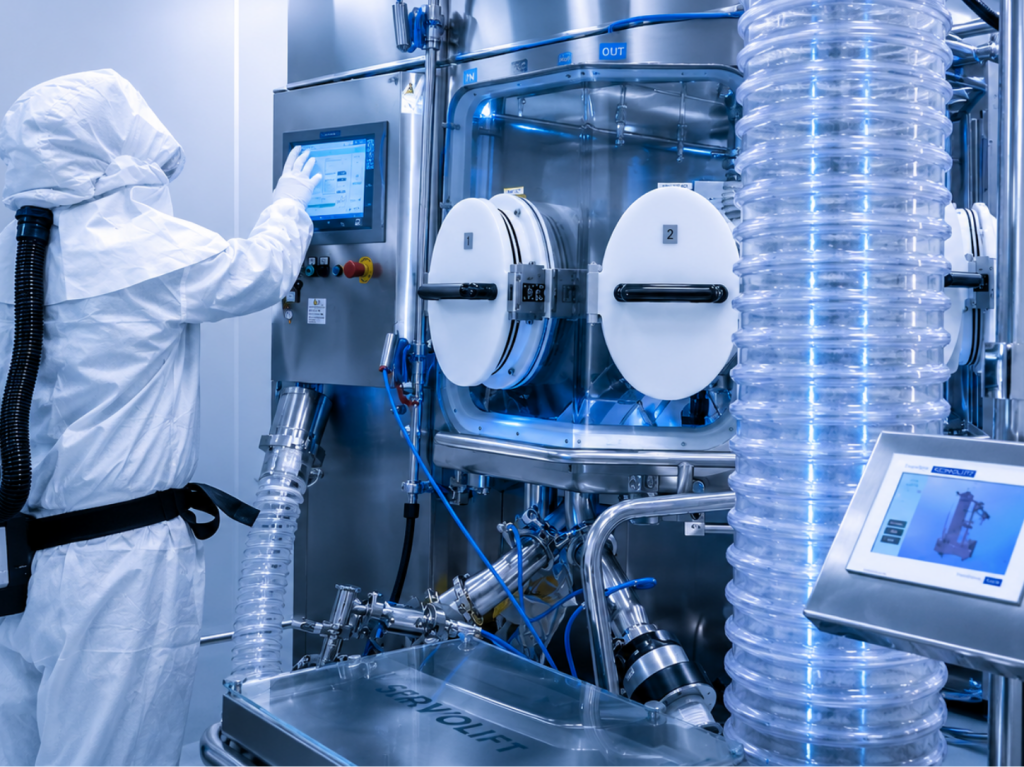
A high-potent, non-sterile plant that produces coated and uncoated tablets and hard gelatin capsules. It uses isolator-based high-containment technology to protect both product and operators.
Home / Capabilities / Manufacture
Delivering world-class pharmaceutical manufacturing through advanced technologies, rigorous quality systems, and continuous innovation to improve patients’ lives.
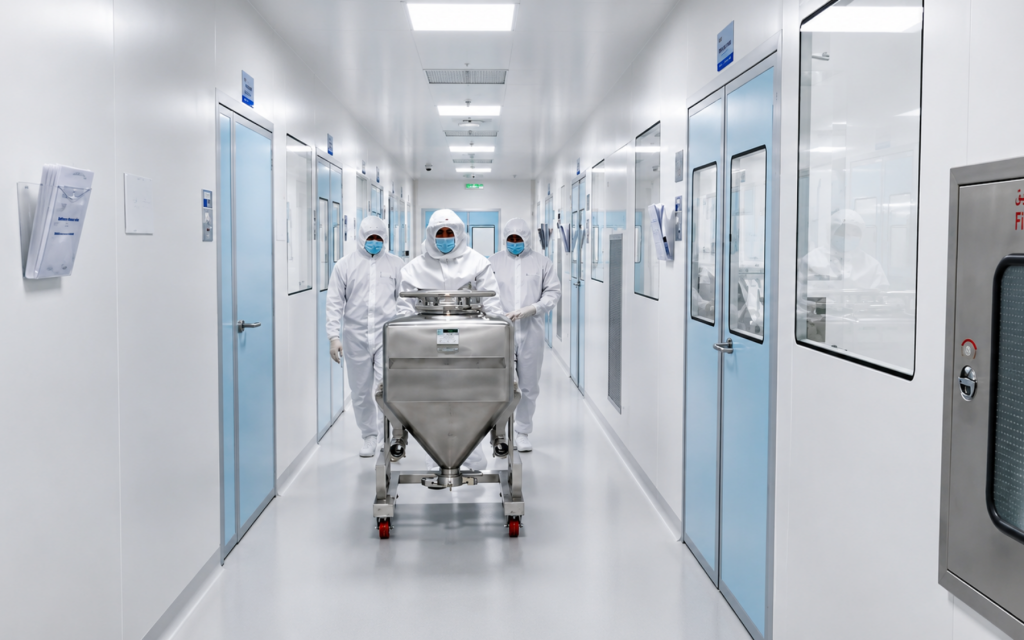
Sudair Pharma operates one of Saudi Arabia's most advanced pharmaceutical manufacturing facilities, designed to produce high-quality medicines that meet international regulatory standards. Our manufacturing ecosystem combines cutting-edge technologies, highly qualified professionals, and efficient production systems to ensure safe, reliable, and scalable pharmaceutical production.
At the heart of Sudair Pharma's operations is a specialized oncology manufacturing plant designed to produce highly technical pharmaceutical products, positioning the company as the first Saudi oncology-specialized manufacturer with its own production facility in the Kingdom. Production Area: 2,853 m²; Storage Area: 1,849 m²; Cold Rooms: 800 m².
Production is organized across multiple dosage-form lines, each with its own defined capacity.
A high-potent, non-sterile plant that produces coated and uncoated tablets and hard gelatin capsules. It uses isolator-based high-containment technology to protect both product and operators.
Produces aseptically processed small-volume injectables, both liquid and lyophilized (freeze-dried). Isolator-based high containment and a Water for Injection (WFI) system support product safety and sterility assurance.
Manufactures and packs general-formulary tablets and capsules, extending our range of locally produced medicines beyond high-potent products.
Expanding our advanced manufacturing capabilities to meet the evolving needs of healthcare and improve patient outcomes.
An insulin manufacturing initiative is underway, progressing in phases from secondary packaging to full compounding, filling, and formulation. Commercial activity is increasing, with full-scale manufacturing targeted for 2028.
A biosimilars and monoclonal antibodies facility is being developed,covering purification, aseptic filling, and quality control aligned with EMA, FDA, and SFDA standards. The facility targets biologics development in oncology, immunology, and chronic disease treatment.
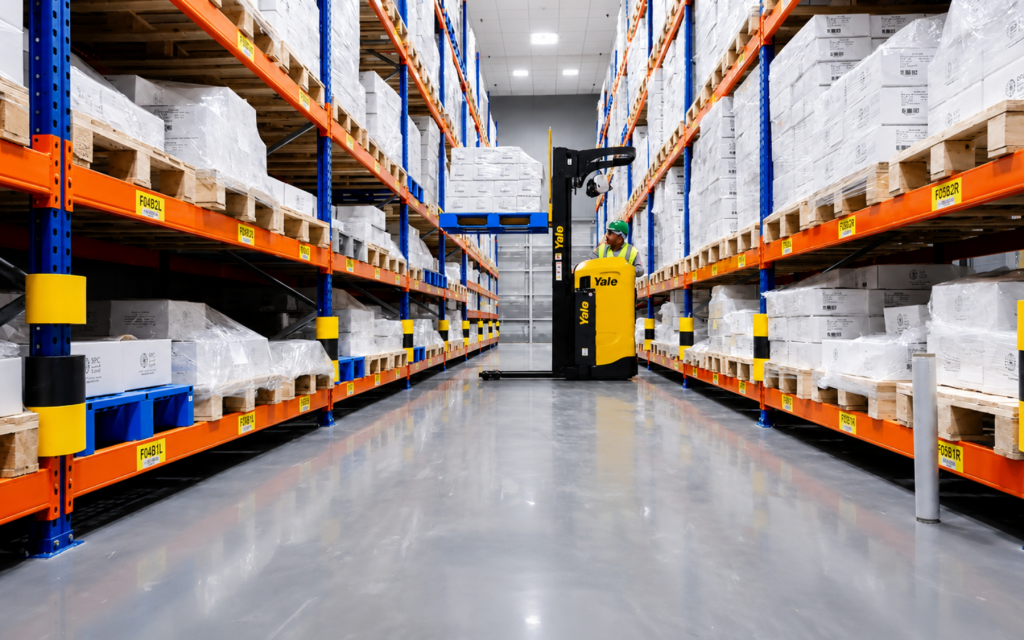
A respiratory manufacturing facility is also planned. The facility is intended to produce dry-powder inhalers, metered-dose inhalers, soft-mist devices, and sterile nebulized solutions for chronic respiratory condition.
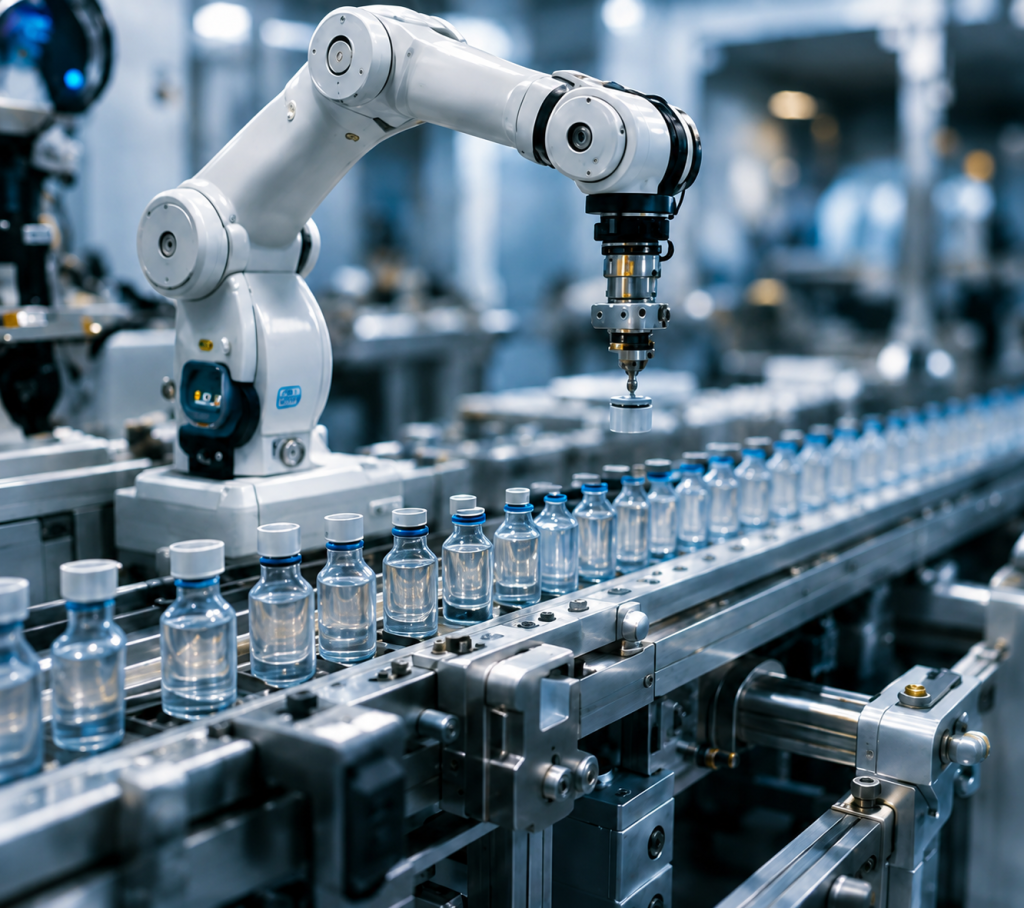
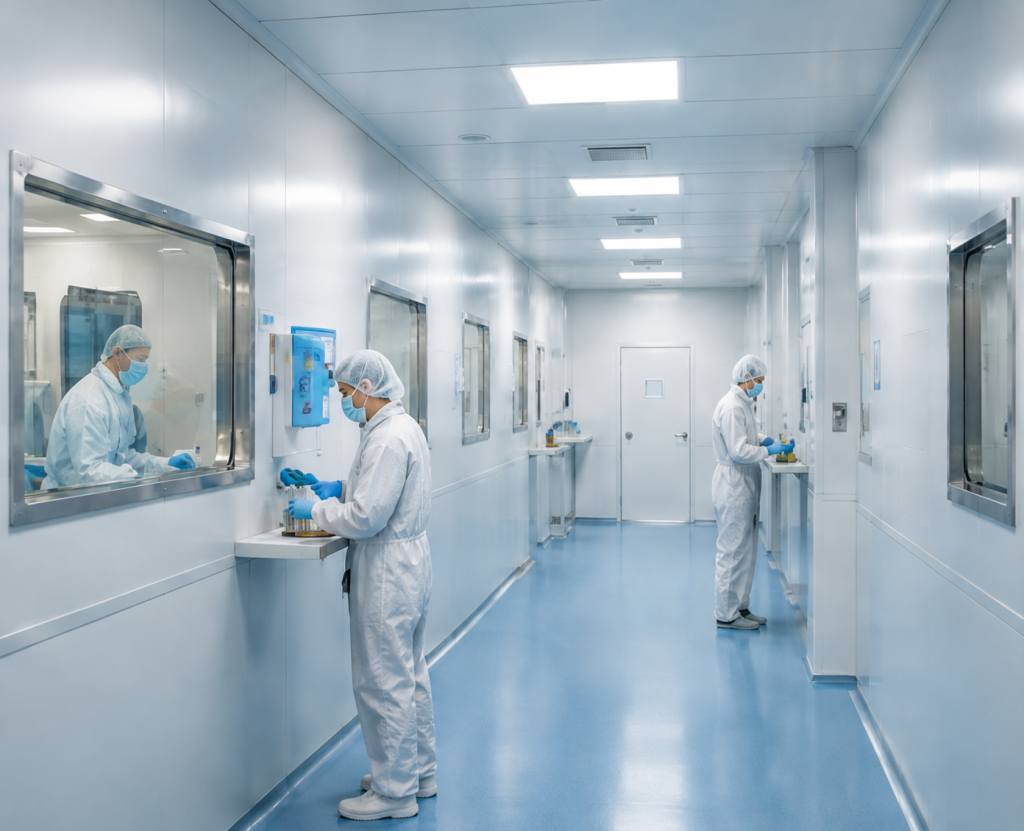
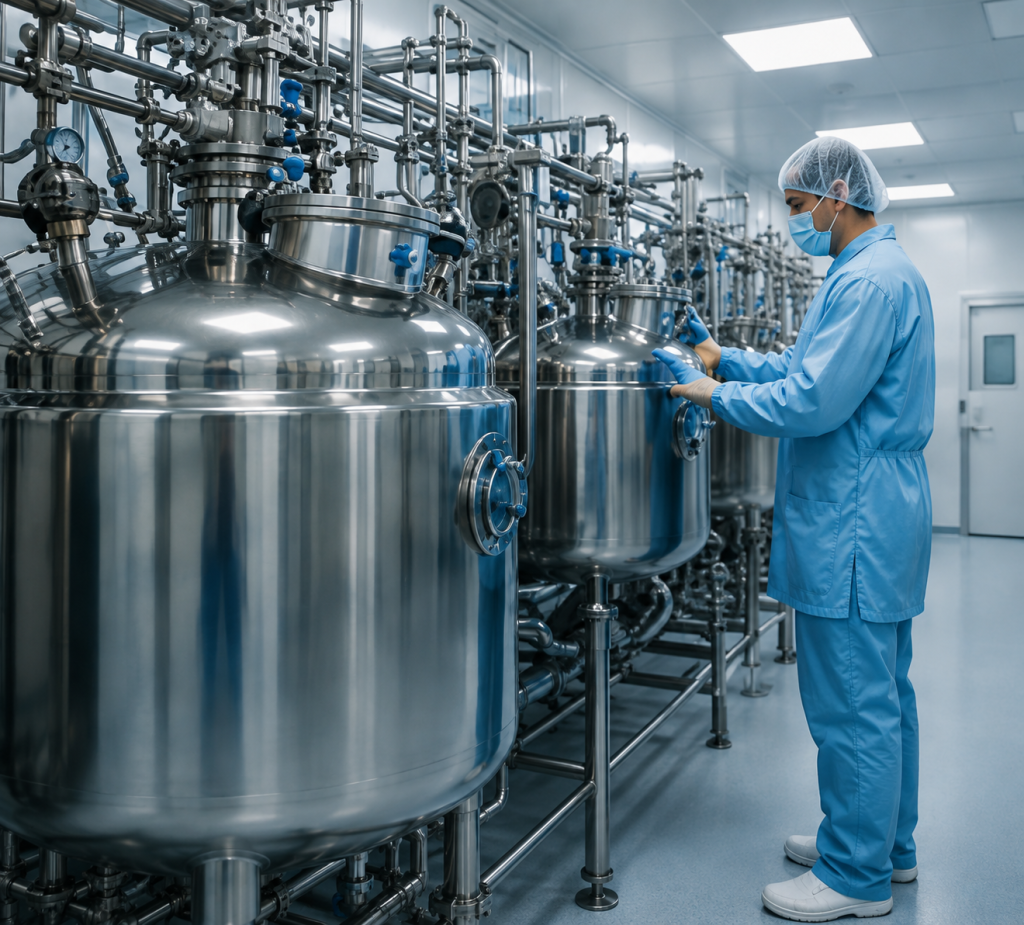
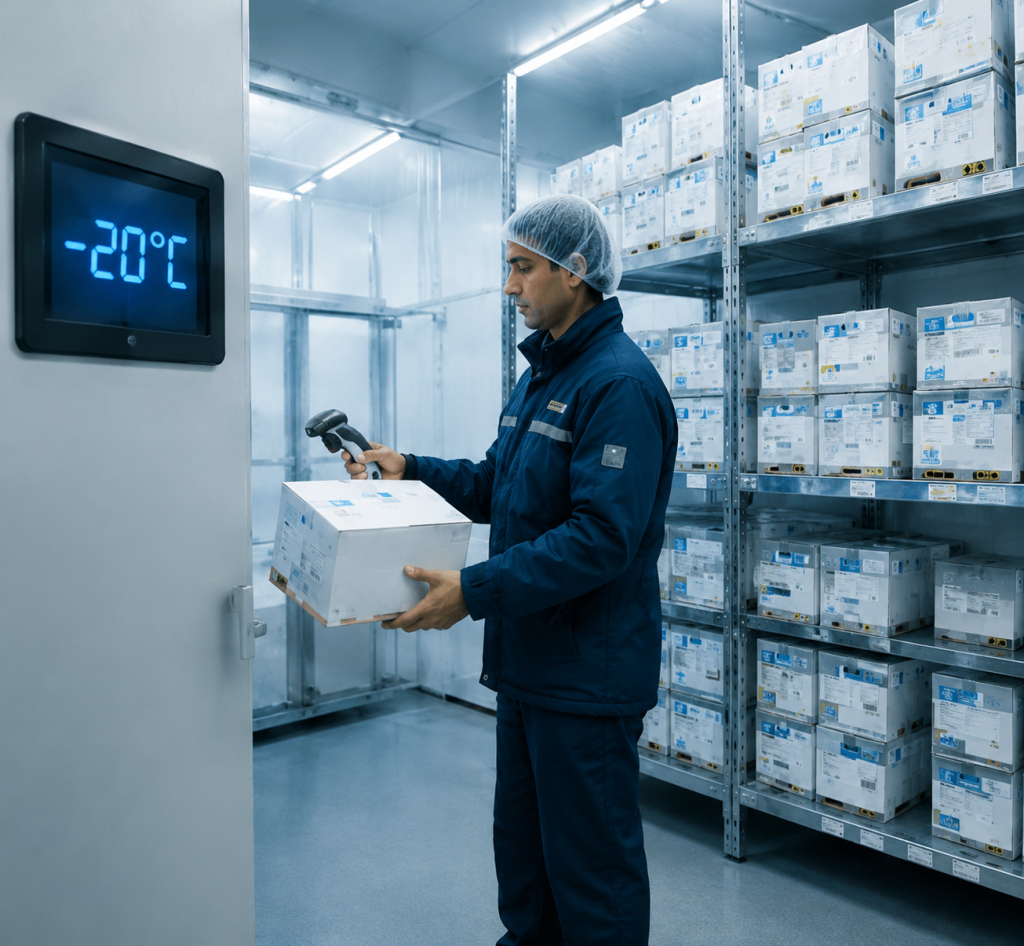
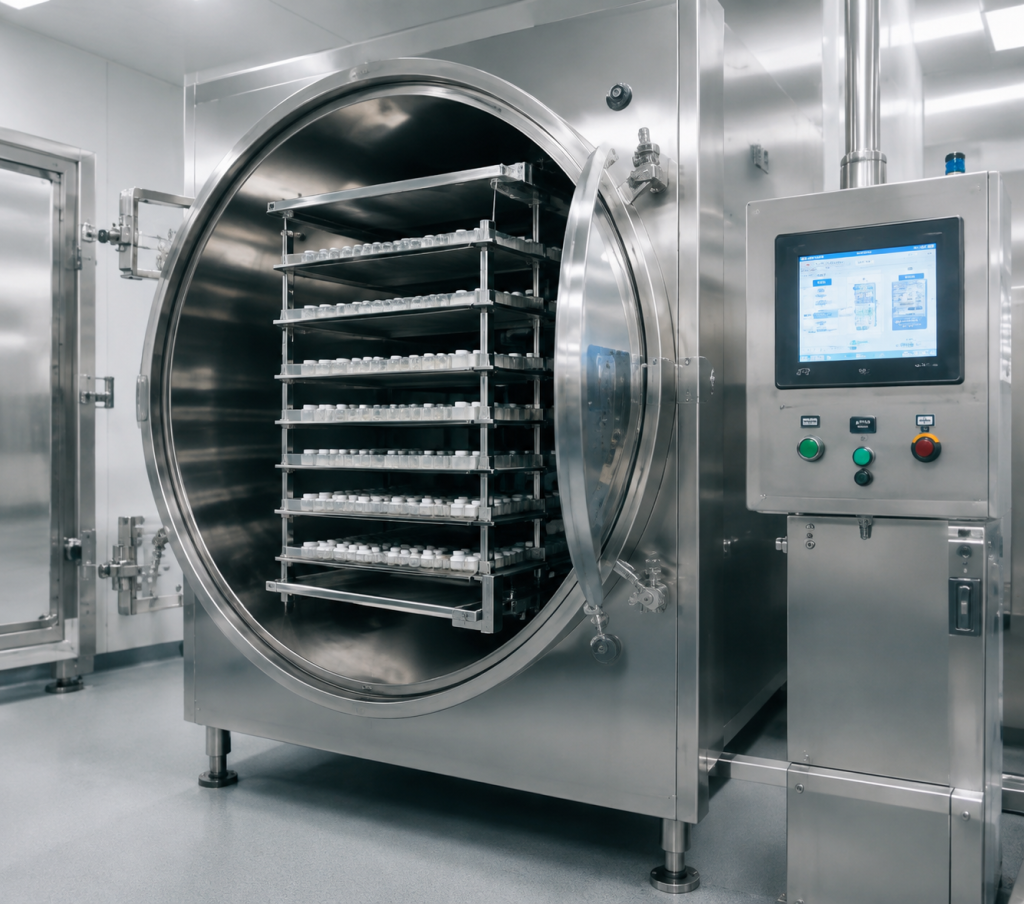
Specialized facilities, validated processes, and production built to international standards.